Introduction
Semiconductor packages are becoming smaller, denser, and more structurally complex as electronics manufacturers adopt advanced packaging, finer interconnects, stacked dies, miniaturized wire bonds, micro-bumps, and other high-density structures. At the same time, inspection requirements are moving beyond simple visual defect detection.
For engineers working in semiconductor packaging, a package may need to be inspected for much more than surface appearance. Critical features can include wire diameter, bond position, pad spacing, solder ball diameter, package dimensions, component height, step height, coplanarity, surface profile, and other geometric characteristics.
This is where a measuring microscope for semiconductor package inspection becomes useful.
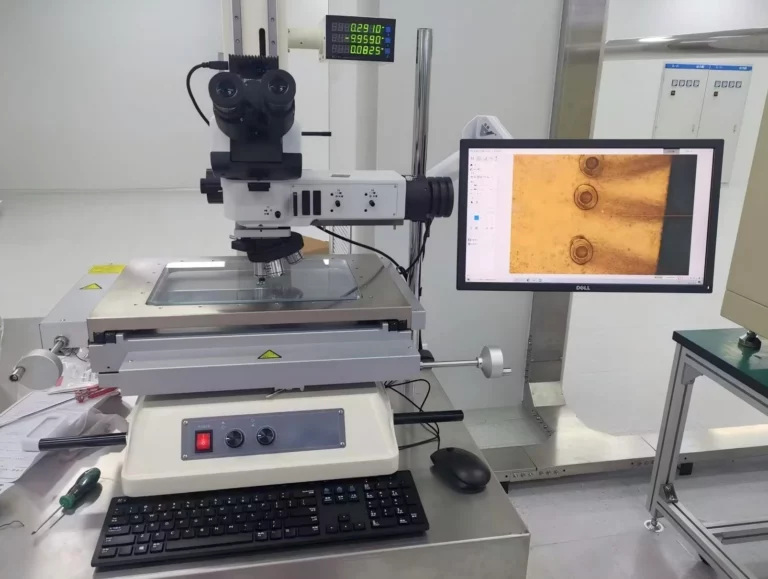
Unlike a conventional inspection microscope, which is primarily designed to provide magnified visual observation, a measuring microscope combines high-resolution imaging, calibrated measurement, precision positioning, and measurement software. Depending on its configuration, it can perform 2D dimensional measurement as well as height, depth, and 3D surface analysis.
For semiconductor packaging applications, the key question is therefore not simply “How much magnification does the microscope provide?” A more useful question is:
What package features need to be measured, in which dimension, and with what repeatability?
For a broader overview of optical measurement solutions, explore our measuring microscope solutions for precision dimensional measurement, including systems designed for accurate 2D and 3D inspection applications.
This article explains how measuring microscopes are applied to semiconductor package inspection, which package features can be measured, when XYZ or 3D measurement is required, and what engineers should consider when selecting an optical measurement system.
Table of Contents
What Is a Measuring Microscope for Semiconductor Package Inspection?
A measuring microscope for semiconductor package inspection is an optical measurement system designed to magnify semiconductor package structures while providing calibrated dimensional measurements.
In a typical system, the microscope combines:
- High-resolution optical imaging
- A digital camera or imaging sensor
- Precision X-Y or XYZ positioning
- Calibrated measurement software
- Adjustable illumination
- Measurement and reporting functions
Depending on the system architecture, engineers can measure parameters such as:
| Measurement | Semiconductor Package Example |
|---|---|
| Length | Package body, lead, die or bonding structure |
| Width | Wire, pad, lead or package feature |
| Diameter | Wire bond, solder ball, hole or circular feature |
| Distance | Bond-to-pad spacing, terminal pitch |
| Angle | Bond wire or package edge angle |
| Position | Bonding point or component location |
| Height | Wire loop, solder ball, package step |
| Depth | Groove, recess or cavity |
| Step height | Difference between package surfaces |
| Profile | Cross-sectional geometry or surface contour |
| Coplanarity | Relative height of terminals or solder balls |
The exact measurement capability depends on the optical configuration, stage, calibration method, image processing algorithms, and whether the system provides 2D or 3D measurement.
This distinction is important because a high-magnification microscope is not automatically a measuring microscope. Magnification makes a feature easier to see, but calibrated positioning and measurement algorithms are required to convert what is visible into quantitative dimensional data.
Why Semiconductor Package Inspection Requires Dimensional Measurement
Visual inspection remains an important part of semiconductor quality control, but it does not answer every engineering question.
Consider a wire bond that appears visually normal under magnification. An engineer may still need to determine:
- Is the wire diameter within specification?
- Is the bonding position correct?
- Is the distance between bonding points consistent?
- Is the loop height within the process window?
- Has the wire shifted after bonding?
- Are adjacent structures maintaining sufficient clearance?
The same principle applies to solder balls and package terminals. A visual image may reveal contamination, deformation, cracks, or obvious defects, but dimensional measurement provides quantitative information that can be compared against drawings, process specifications, or inspection criteria.
This is particularly relevant as semiconductor packaging moves toward finer structures.
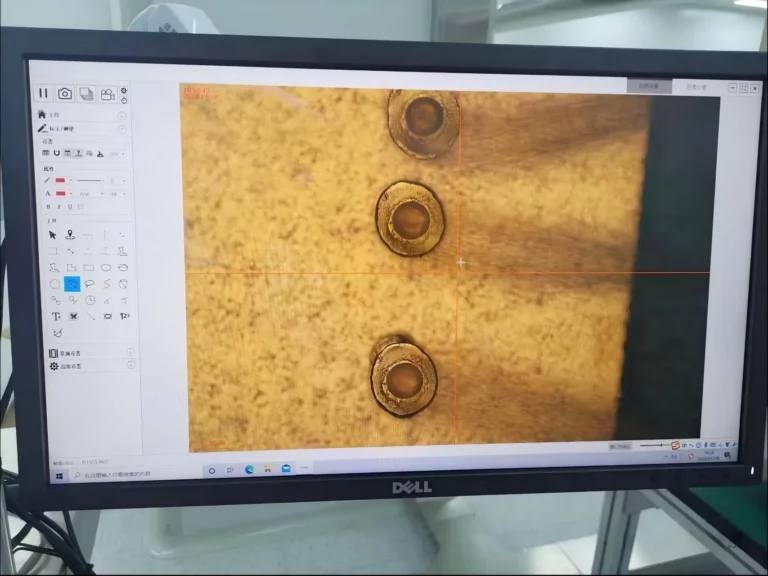
For example, one advanced packaging manufacturer reports capabilities involving 15–38 µm wire diameters, minimum die-pad bonding pitch of 35 µm, and pitches down to 50 µm for certain advanced packaging processes. These dimensions illustrate why optical inspection systems increasingly need both high-resolution imaging and reliable measurement capability.
The inspection requirement is therefore not simply “see the wire.” It may be necessary to see, locate, measure, compare, and document the wire geometry.
What Can a Measuring Microscope Measure on a Semiconductor Package?
The measurable features depend on package type and microscope configuration, but most semiconductor package inspection tasks can be divided into several categories.
1. Wire Bond Measurement
Wire bonding is one of the most common applications for high-resolution optical measurement.
A measuring microscope can be used to evaluate:
- Wire diameter
- Bonding point position
- Bond-to-bond distance
- Wire spacing
- Loop geometry
- Bond pad dimensions
- Bonding angle
- Clearance between adjacent wires
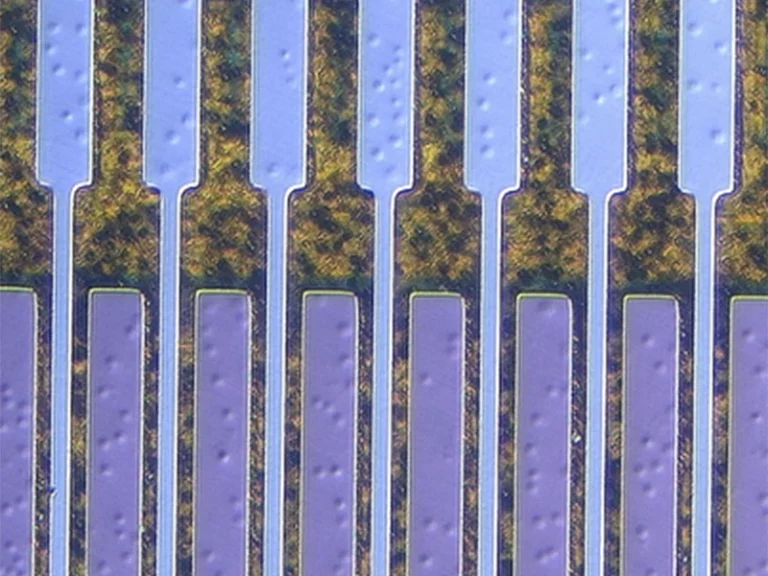
Wire diameters can reach only a few tens of micrometers in some advanced packaging applications. For this reason, measurement accuracy, optical resolution, image contrast, and edge detection all become important.
A system with an XYZ stage can also provide controlled positioning when multiple bonding points need to be measured across the same package.

2. Solder Ball and BGA Measurement
BGA and other area-array packages introduce another group of dimensional inspection requirements.
Typical measurements include:
- Solder ball diameter
- Ball-to-ball spacing
- Ball position
- Ball height
- Ball deformation
- Surface-to-ball height difference
- Package-to-terminal alignment
For 2D measurements, the microscope can measure diameter, pitch, and position from calibrated images.
However, if the engineering question involves ball height or height variation, a conventional 2D image is insufficient. A 3D or height-measurement method becomes more appropriate.
This is one reason semiconductor package inspection increasingly combines optical imaging with metrology functions.

3. Package Body and Component Dimensions
A measuring microscope can also be used to verify external package geometry.
Depending on package type, engineers may measure:
- Package length and width
- Lead dimensions
- Terminal spacing
- Die dimensions
- Exposed pad dimensions
- Package edge position
- Feature-to-feature distance
- Small mechanical structures
These measurements can be useful during incoming inspection, process verification, R&D, failure analysis, and production quality control.
JEDEC Standard No. 9C, for example, establishes inspection criteria for microelectronic packages and covers optical inspection of package conditions. It specifies examination at 1.5X to 10X magnification, with higher magnification allowed for evaluating anomalies.
The important distinction is that inspection magnification and dimensional measurement are related but not identical requirements. A standard may specify an observation magnification, while the measurement system must additionally provide calibrated dimensional data.
4. Package Height, Step Height and Surface Profile
Many semiconductor packages contain multiple vertical levels.
For example, an engineer may need to evaluate the height difference between:
- Package body and substrate
- Die and substrate
- Solder ball and package surface
- Bond wire and package surface
- Raised and recessed structures
- Different levels of an advanced package
These are fundamentally Z-axis measurement problems.
A standard 2D measuring microscope can provide excellent X-Y measurements, but a top-view image alone cannot reliably determine the actual vertical distance between two surfaces.
A 3D measuring microscope can instead use focus information, optical reconstruction, or other non-contact measurement techniques to generate a surface profile and calculate height differences.
This distinction becomes particularly important for semiconductor packages with uneven or multi-level structures.
Measuring Microscope vs. Inspection Microscope for Semiconductor Packages
A conventional inspection microscope and a measuring microscope may look similar from the outside, but their intended functions are different.
| Capability | Inspection Microscope | Measuring Microscope |
| Magnified observation | ✓ | ✓ |
| Defect observation | ✓ | ✓ |
| Calibrated 2D measurement | Limited / optional | ✓ |
| X-Y positioning | Usually basic | Precision stage |
| Automatic edge detection | Usually unavailable | Often available |
| Length / width measurement | Limited | ✓ |
| Diameter / pitch measurement | Limited | ✓ |
| Height measurement | Usually unavailable | Depending on configuration |
| Depth measurement | Usually unavailable | Depending on configuration |
| 3D surface measurement | Usually unavailable | Advanced systems |
| Measurement reports | Limited | ✓ |
| Quantitative process analysis | Limited | ✓ |
The difference can be summarized simply:
An inspection microscope answers “What does the package look like?” A measuring microscope answers “What is the measured dimension of the feature?”
For semiconductor manufacturing, both functions can be valuable, but the required system depends on whether the inspection process is primarily visual or metrological.
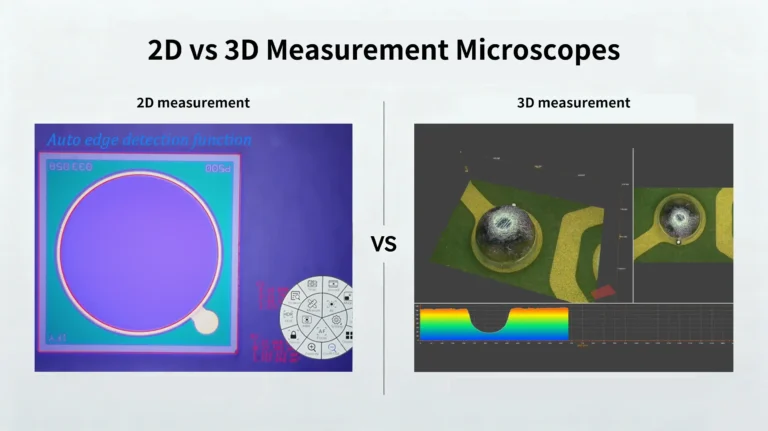
2D vs. 3D Measurement for Semiconductor Package Inspection
One of the most important decisions when selecting a measuring microscope is whether the application requires 2D measurement or 3D measurement.
2D Measurement
2D measurement analyzes dimensions visible on the image plane.
Typical measurements include:
- Length
- Width
- Diameter
- Radius
- Angle
- Pitch
- Center-to-center distance
- Area
- X-Y position
For example, measuring the diameter of a wire bond or the spacing between two bonding pads is fundamentally a 2D measurement task when the relevant geometry lies in the image plane.
3D Measurement
3D measurement becomes necessary when the feature’s vertical geometry matters.
Typical applications include:
- Package height
- Solder ball height
- Wire loop height
- Step height
- Groove depth
- Surface profile
- Warpage-related surface analysis
- Height variation across a package
The distinction can be expressed as follows:
| Inspection Requirement | Recommended Measurement |
| Wire diameter | 2D |
| Bond pad width | 2D |
| Bonding point position | 2D |
| Terminal pitch | 2D |
| Package length and width | 2D |
| Solder ball diameter | 2D |
| Solder ball height | 3D / Z measurement |
| Wire loop height | 3D / Z measurement |
| Package step height | 3D / Z measurement |
| Groove depth | 3D / Z measurement |
| Surface profile | 3D |
| Package surface height variation | 3D |
This is also why an XYZ measuring microscope can be more versatile than an XY-only system when semiconductor packages contain significant height variation. The choice between 2D and 3D measurement ultimately depends on the geometry of the feature being inspected and whether height information is required. For a detailed comparison, see 2D vs 3D Measurement Microscopes: What Is the Difference?

Why the Z Axis Matters in Semiconductor Package Inspection
The X and Y axes describe lateral position:
- X: left-to-right movement
- Y: front-to-back movement
The Z axis describes vertical movement.
For semiconductor package inspection, Z-axis information can be used to determine the height difference between two surfaces or to locate the focus position associated with different structural levels.
For example, suppose a package contains a raised structure with a nominal height of 120 µm above a reference surface. A 2D image can show the structure’s width and position, but it does not directly provide its 120 µm vertical dimension.
With an appropriate 3D measuring system, the engineer can establish a reference plane and calculate the height difference between the two surfaces.
This becomes especially useful when inspecting:
- Die attach structures
- Wire loops
- Solder balls
- Bumps
- Package steps
- Microvias
- Recessed features
- Surface profiles
The measurement principle is simple, but the actual accuracy depends on optical resolution, calibration, mechanical stability, surface reflectivity, illumination, reconstruction method, and sample geometry.
Semiconductor Package Inspection Challenges for Optical Measurement
Semiconductor packages are not always easy optical samples.
Several factors can affect measurement reliability.
Reflective Metal Surfaces
Gold, copper, aluminum, nickel, solder, and other metallic surfaces can produce strong reflections.
If the camera receives excessive reflected light, edges may become saturated or blurred. This can affect automatic edge detection and therefore dimensional measurement.
Adjustable brightfield, darkfield, coaxial, or polarized illumination can help improve contrast depending on the surface.
Multi-Level Structures
A package can contain several structures at different heights.
At high magnification, conventional optical systems have limited depth of field. As a result, focusing on one level may leave another level blurred.
Extended Depth of Field (EDF) or focus-stacking technology can combine multiple focal planes into a fully focused image. This is particularly useful when the inspection target includes wire bonds, solder joints, steps, grooves, or other uneven structures.
Small Features
As features approach tens of micrometers, optical resolution becomes increasingly important.
For context, semiconductor inspection equipment currently available for advanced packaging includes systems with stated resolutions of approximately 2.5 µm, with applications including wire bonding, die bonding, bumps, and solder joints. Other systems specify 3 µm or 5.5 µm high-resolution inspection platforms for semiconductor packaging.
These figures should not be interpreted as universal measurement accuracy. Optical resolution, stage resolution, repeatability, calibration accuracy, and final measurement accuracy are different specifications.
This is an important point when evaluating a measuring microscope.
Coplanarity and Package Warpage: When Measurement Goes Beyond Simple Dimensions
Semiconductor package inspection may also involve coplanarity and warpage, particularly for surface-mount packages.
JEDEC JESD22-B108 addresses coplanarity testing for surface-mount semiconductor devices and defines the purpose as measuring the deviation of terminals, including leads or solder balls, from coplanarity.
Package warpage is another important consideration during board assembly. JEDEC JESD22-B112C is specifically intended to measure deviation from uniform flatness of surface-mount integrated circuit packages under elevated-temperature conditions associated with soldering.
This illustrates an important limitation:
A room-temperature optical measuring microscope should not automatically be treated as a complete replacement for a dedicated thermal warpage measurement system.
For routine dimensional inspection, optical measurement can be highly useful. For standardized elevated-temperature warpage characterization, however, the measurement method, temperature control, fixture, and applicable standard must all be considered.
This distinction is particularly important for engineers specifying inspection equipment or for companies providing semiconductor measurement services.
Measuring Microscope for Semiconductor and Fiber Optic Inspection
Semiconductor packaging and fiber-optic components share several inspection requirements: small structures, precise alignment, polished or reflective surfaces, and the need for repeatable dimensional analysis.
For applications involving optical connectors, fiber alignment structures, ferrules, and other miniature optical components, see our dedicated guide to semiconductor and fiber optic inspection microscopes.
The appropriate microscope configuration can differ significantly depending on whether the main task is package dimensional measurement, fiber alignment, surface defect inspection, or 3D geometry analysis.
How to Choose a Measuring Microscope for Semiconductor Package Inspection
The microscope should be selected according to the measurement task, rather than magnification alone.
Key specifications to evaluate include:
| Specification | Why It Matters |
| Optical resolution | Determines how closely spaced features can be visually resolved |
| Measurement accuracy | Indicates how close measured values are to the actual dimension |
| Repeatability | Indicates consistency when the same feature is measured repeatedly |
| XY stage resolution | Important for precise lateral positioning |
| Z-axis resolution | Important for height and depth measurement |
| Magnification range | Determines the range of feature sizes that can be inspected |
| Working distance | Important for tall packages and accessories |
| Illumination | Affects contrast and edge detection |
| EDF / focus stacking | Useful for uneven package structures |
| 3D reconstruction | Required for surface and height analysis |
| Calibration | Essential for quantitative measurement |
| Measurement software | Determines available measurement and reporting functions |
A useful selection workflow is:
Define the feature → define the required dimension → determine 2D or 3D → specify required accuracy/repeatability → select optics and stage → validate the system with actual samples.
This is generally more reliable than selecting a microscope based only on its maximum magnification.
Conclusion
A measuring microscope for semiconductor package inspection is most useful when semiconductor inspection requires quantitative dimensional information rather than visual observation alone.
For 2D package inspection, engineers can measure wire diameter, pad dimensions, terminal spacing, solder ball diameter, pitch, angles, and feature positions. When package geometry includes significant height variation, an XYZ or 3D measuring microscope can additionally evaluate height, depth, step height, and surface profiles.
The growing complexity of semiconductor packaging makes this distinction increasingly important. Features measured in tens of micrometers, reflective materials, multi-level structures, and tight dimensional tolerances all place greater demands on optical measurement systems.
At the same time, measurement accuracy should always be evaluated as a system-level specification. Optical resolution, stage resolution, calibration accuracy, repeatability, illumination, software, and sample characteristics all influence the final measurement result.
For engineers, semiconductor manufacturers, inspection laboratories, optical instrument distributors, and technical service providers, the most appropriate measuring microscope is therefore the one that matches the actual measurement task—not simply the system with the highest magnification.