Introduction
When selecting a microscope for electronics inspection, semiconductor analysis, or precision manufacturing, one of the most common questions engineers ask is:
“Should we choose higher magnification or Extended Depth of Field (EDF) technology to improve inspection accuracy?”
At first glance, higher magnification seems like the obvious answer. A larger image appears to reveal more details, making it easier to identify solder defects, surface damage, or microscopic structures.
However, in real-world inspection environments, magnification is only one part of image quality.
For three-dimensional objects such as PCB assemblies, semiconductor packages, connectors, and precision mechanical components, depth of field (DoF) often becomes the actual limitation. A microscope may provide extremely high magnification, but if only a small portion of the object remains in focus, important inspection information can still be lost.
For applications involving complex surfaces and height variations, many engineers are turning to Extended Depth of Field microscope technology, which combines multiple focal planes into a single fully focused image. This approach allows inspectors to evaluate multiple levels of a component simultaneously rather than repeatedly adjusting focus.
For a deeper understanding of how this technology is applied in industrial inspection, an Extended Depth of Field microscope provides a practical solution for applications requiring clear imaging across different heights, including PCB inspection, semiconductor packaging, and precision component analysis.
This article compares EDF technology and higher magnification microscopy, explaining how each affects inspection accuracy and when engineers should prioritize one over the other.
Table of Contents
The Common Misconception: Why Higher Magnification Does Not Always Mean Better Inspection
Magnification Shows More Detail, But It Does Not Guarantee Better Inspection
Magnification refers to how much larger an object appears through the microscope compared with viewing it directly.
For example:
- 10X magnification makes an object appear ten times larger.
- 50X magnification provides a much closer view of surface details.
- 100X magnification allows observation of extremely small structures.
However, magnification alone does not determine whether an inspection result is accurate.
A high-magnification microscope may reveal:
- Smaller solder defects
- Fine surface scratches
- Micro cracks
- Contamination particles
But it may also introduce challenges:
- Narrow field of view
- Reduced depth of field
- Increased focusing difficulty
- More frequent operator adjustments
In manufacturing environments, inspection accuracy depends on whether engineers can clearly evaluate the entire feature of interest, not just whether the image is enlarged.
For example, when inspecting a BGA package, a connector, or a tall capacitor, engineers may need to observe:
- Top surface condition
- Sidewall structure
- Solder connection area
- Surrounding components
A higher magnification image that only keeps one area sharp may provide less useful information than a lower magnification image where the complete structure is clearly visible.
Understanding the Relationship Between Magnification, Resolution, and Depth of Field
Magnification vs Resolution: Two Different Optical Concepts
A common misunderstanding is treating magnification and resolution as the same thing.
They are different optical parameters.
Magnification determines image size.
Resolution determines the ability to distinguish two closely spaced details.
A microscope with high magnification but poor optical resolution simply enlarges an unclear image.
In industrial inspection, resolution depends on multiple factors:
- Optical quality
- Numerical aperture (NA)
- Sensor performance
- Illumination quality
- Image processing capability
For digital microscope systems, camera resolution has also become an important factor.
Modern industrial inspection cameras commonly use sensors from approximately:
- 2 MP for basic viewing
- 5–12 MP for general inspection
- 20 MP or higher for detailed documentation and measurement applications
However, increasing sensor resolution does not solve depth limitations.
A high-resolution camera can capture more pixels, but if different areas of the object are located outside the focus range, those details will still appear blurred.
Why Increasing Magnification Reduces Depth of Field
One of the fundamental limitations of optical microscopy is that depth of field decreases as magnification increases.
The higher the magnification, the thinner the acceptable focus range becomes.
A simplified comparison:
| Magnification | Typical Inspection Use | Depth of Field |
|---|---|---|
| 5X–10X | PCB overview, component placement | Larger |
| 10X–30X | SMT solder inspection | Moderate |
| 30X–80X | Fine defect analysis | Limited |
| 100X+ | Microstructure inspection | Extremely shallow |
This relationship creates a challenge for engineers inspecting three-dimensional objects.
For example:
A PCB connector may have:
- Plastic housing at the top
- Metal pins in the middle
- Solder joints near the PCB surface
At high magnification, these areas may exist across several millimeters of height difference.
A conventional microscope can only focus on one area at a time.
Why Depth of Field Is Often the Real Limitation in Inspection Accuracy
Three-Dimensional Objects Require Three-Dimensional Imaging Solutions
Most industrial inspection targets are not flat.
Examples include:
- PCB assemblies
- Semiconductor packages
- Wire bonding structures
- Precision mechanical parts
- Medical components
These objects contain multiple vertical levels.
When inspecting such components, engineers are often less concerned about seeing a single tiny detail and more concerned about understanding the complete structure.
For example, during solder joint inspection, the important information may include:
- Solder fillet shape
- Wetting area
- Lead position
- Component alignment
- Surrounding clearance
If only one area is focused, the inspection decision becomes incomplete.

The Impact of Manual Refocusing on Inspection Efficiency
With traditional microscopes, operators often compensate for limited depth of field by manually adjusting focus.
This creates several practical problems:
1. Longer Inspection Time
Operators must repeatedly adjust the focus position when moving between different component heights.
2. Reduced Consistency
Different operators may choose different focus points, creating variation in inspection judgment.
3. Documentation Challenges
A single image may not clearly represent the entire structure, making communication and quality reporting more difficult.
4. Higher Training Requirements
Experienced operators often develop techniques to compensate for optical limitations, but this introduces dependence on individual skill.
For electronics manufacturers and inspection service providers, reducing operator dependency is increasingly important as product complexity increases.
Extended Depth of Field (EDF) Technology Explained: How Focus Stacking Improves Inspection Accuracy
What Is Extended Depth of Field (EDF) Microscopy?
Extended Depth of Field (EDF) microscopy is an imaging technology that increases the visible focus range of a microscope by combining multiple images captured at different focus positions.
Unlike a conventional microscope that produces a single focal plane, an EDF microscope captures information from multiple vertical levels and merges the sharp areas into one fully focused image.
The basic principle can be summarized as:
Multiple focal images → Sharpness analysis → Image fusion → Extended focus image
This allows engineers to observe complex three-dimensional structures without continuously adjusting the focus manually.
EDF technology is also commonly known as focus stacking microscopy because it stacks multiple images from different focus layers into a single image with increased depth of field.
For engineers working with PCB assemblies, semiconductor packages, and precision components, this approach solves one of the most common optical problems: how to maintain clarity across objects with different heights.

How Focus Stacking Works in Industrial Microscopy
The focus stacking process typically includes four major steps.
Step 1: Capturing Multiple Focus Layers
The microscope captures a series of images while moving through different Z-axis positions.
For example:
- Image 1 focuses on the PCB surface
- Image 2 focuses on the solder joint
- Image 3 focuses on the component body
- Image 4 focuses on the upper structure
Each image contains different sharp information.
Step 2: Identifying Sharp Regions
The software analyzes each captured image and determines which areas contain the highest level of detail.
Sharp areas usually contain:
- Higher contrast
- Clear edges
- More texture information
Step 3: Combining Images Through Image Fusion
The system extracts the sharp regions from different focus layers and combines them into one image.
The final image provides:
- Extended focus range
- Improved visibility
- More complete structural information
Step 4: Generating Inspection Data
Depending on the microscope system, the final image can be used for:
- Visual inspection
- Measurement
- Documentation
- Defect comparison
- Quality reporting
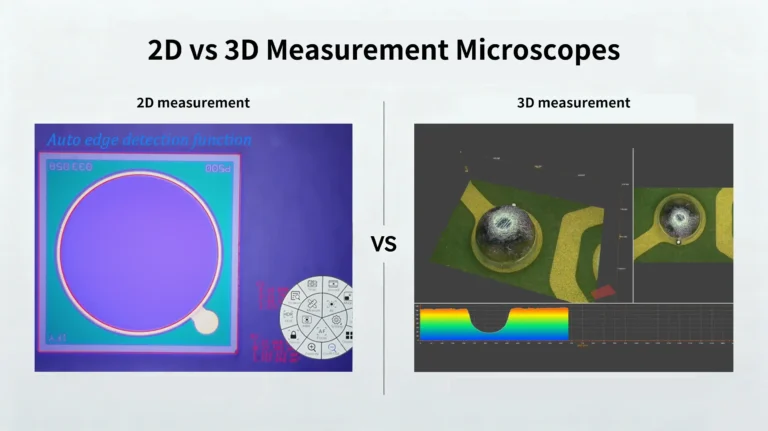
Some advanced systems can also combine EDF imaging with 3D measurement functions to analyze height differences and surface profiles.
Extended Depth of Field (EDF) vs Higher Magnification Microscope: Complete Comparison
Choosing between EDF technology and higher magnification depends on the inspection objective.
A higher magnification microscope is useful when the main requirement is observing extremely small details on relatively flat surfaces.
However, EDF technology becomes more valuable when the inspection target contains height variation.
The following comparison summarizes the practical differences:
| Feature | Higher Magnification Microscope | Extended Depth of Field (EDF) Microscope |
|---|---|---|
| Primary Advantage | Enlarges small details | Keeps multiple heights in focus |
| Image Detail | Excellent at single focus plane | Excellent across multiple planes |
| Depth of Field | Limited | Extended |
| Tall Component Inspection | Difficult | Excellent |
| Manual Refocusing | Frequently required | Greatly reduced |
| PCB Assembly Inspection | Moderate | Excellent |
| Solder Joint Evaluation | Good for flat areas | Better for complex structures |
| Documentation Quality | Depends on focus position | More consistent |
| Operator Skill Dependency | Higher | Lower |
| 3D Structure Observation | Limited | Improved |
| Suitable Applications | Flat micro-details | Complex 3D assemblies |
When Should Engineers Choose EDF Instead of Higher Magnification?
PCB and PCBA Inspection
PCB assemblies are one of the most common applications where EDF provides advantages over simply increasing magnification.
Modern PCBAs often contain:
- Fine-pitch IC packages
- Tall connectors
- Electrolytic capacitors
- Power inductors
- Shield covers
- Through-hole components
These structures may have height differences from several millimeters to several centimeters.
During inspection, engineers often need to evaluate multiple areas simultaneously:
- Component placement
- Solder quality
- Lead alignment
- Mechanical clearance
- Surface condition
A high-magnification microscope may show excellent detail on one area but require repeated focusing.
EDF imaging provides a more complete inspection view.

Semiconductor Package Inspection
Semiconductor inspection is another area where depth information is critical.
Common inspection tasks include:
- BGA solder ball inspection
- Wire bonding evaluation
- Package surface inspection
- Die and substrate analysis
For example, BGA packages contain structures distributed across different height levels.
Engineers may need to observe:
- Solder ball shape
- Package edge condition
- Surface defects
- Bonding structures
EDF technology helps maintain image clarity across these different areas.

Precision Manufacturing and Industrial Inspection
Beyond electronics, EDF microscopy is also useful for precision manufacturing applications.
Examples include:
- Machined micro parts
- Medical components
- Precision connectors
- Optical components
- Surface defect inspection
In these applications, the inspection target is often three-dimensional, meaning depth information is as important as surface detail.
A Practical Decision Guide: Magnification or EDF?
Instead of asking:
“Should we buy the highest magnification microscope?”
engineers should ask:
“What information must be captured during inspection?”
The following guide provides a practical selection approach:
| Inspection Requirement | Recommended Solution |
|---|---|
| Viewing small flat surface defects | Higher Magnification Microscope |
| Inspecting PCB solder joints | Digital / EDF Microscope |
| Inspecting tall components | EDF Microscope |
| Comparing multiple height levels | EDF Microscope |
| Measuring height differences | 3D Measuring Microscope |
| Recording inspection images | EDF Digital Microscope |
| Manual repair work | Stereo Microscope |
Why Combining EDF Imaging with Measurement Capability Provides More Value
Visual inspection answers:
“What does the component look like?”
Measurement answers:
“What is the actual size, height, or dimensional difference?”
For many advanced manufacturing processes, both types of information are required.
Examples include:
- Semiconductor packaging verification
- PCB process improvement
- Connector manufacturing
- Precision assembly inspection
A modern inspection workflow increasingly combines:
- High-resolution imaging
- Extended depth of field
- Measurement software
- Image documentation
- Data reporting
This allows engineers to move from subjective visual evaluation toward more repeatable, data-supported inspection decisions.
For applications requiring both clear imaging and dimensional analysis, understanding focus stacking microscopy principles can help engineers select the appropriate optical system and inspection workflow.
Why Depth of Field Matters in Modern Quality Inspection
Industry inspection guidelines, including principles described in IPC workmanship standards, emphasize that solder joint evaluation requires clear observation of important features such as wetting, fillet formation, component alignment, and connection quality.
These features are not always located on the same optical plane.
For traditional microscopy, inspectors must manually balance magnification, working distance, and focus position. As electronic assemblies become more compact and three-dimensional, this approach becomes increasingly challenging.
EDF microscopy does not replace optical resolution; instead, it solves a different problem by extending the usable focus range.
The most effective inspection systems often combine:
- Appropriate magnification
- High-quality optics
- Optimized illumination
- Extended depth imaging
- Measurement capability
The goal is not simply to make the image larger, but to capture the information required for accurate engineering decisions.
Conclusion
The choice between Extended Depth of Field (EDF) technology and higher magnification depends on the nature of the inspection task.
Higher magnification remains valuable when engineers need to examine extremely small details on relatively flat surfaces. However, magnification alone cannot solve the challenges created by three-dimensional structures and height variations.
For PCB assemblies, semiconductor packages, and complex industrial components, depth of field often has a greater impact on inspection accuracy than magnification.
EDF microscopes improve inspection efficiency by combining multiple focus layers into a single clear image, reducing manual refocusing and providing a more complete view of complex structures.
When selecting an industrial microscope, engineers should evaluate the entire inspection requirement:
- Required detail level
- Component geometry
- Height variation
- Documentation needs
- Measurement requirements
The best microscope is not always the one with the highest magnification. In many modern inspection applications, the ability to maintain focus across the complete structure is what truly improves inspection accuracy.