Introduction
Modern PCB assemblies are becoming increasingly complex. A single board may contain ultra-small SMD components, fine-pitch IC packages, large electrolytic capacitors, power inductors, connectors, shielding covers, and mechanical structures with significant height differences.
This creates a major challenge for optical inspection: keeping both low-level solder joints and tall components completely in focus at the same time.
For engineers performing PCB quality inspection, the problem is not always insufficient magnification. In many cases, the real limitation is depth of field (DoF). A conventional microscope may provide excellent image detail at one focal plane, but areas several millimeters above or below that plane quickly become blurred.
The best microscope for inspecting tall components on PCBs is usually not simply the one with the highest magnification. Instead, engineers should look for a system that combines:
- Extended Depth of Field (EDF) or focus stacking technology
- Long working distance optics
- Flexible viewing angles
- Large field of view
- Accurate measurement capability
An Extended Depth of Field microscope captures multiple images at different focus positions and combines the sharp regions into one fully focused image. This makes it particularly suitable for inspecting PCBA assemblies with large height variations, such as connectors, capacitors, power modules, and stacked electronic structures.
For applications requiring detailed PCB inspection, engineers often choose specialized extended depth of field microscopes because they provide clearer visualization of complex three-dimensional structures compared with traditional optical inspection methods.
This guide explains why tall PCB components are difficult to inspect, which microscope features matter most, and how to select the right inspection solution for modern electronics manufacturing.
Table of Contents
The Optical Dilemma: Why Inspecting Tall Components Is Hard
The High-Aspect-Ratio Challenge in PCB Inspection
The main difficulty when inspecting tall PCB components comes from the difference between component height and microscope depth of field.
A typical PCB assembly may contain:
- 0.5 mm pitch semiconductor packages
- 3–5 mm passive components
- 10–30 mm electrolytic capacitors
- 15–40 mm connectors or transformers
- Large mechanical parts exceeding 50 mm
These different structures create a high-aspect-ratio inspection environment where the microscope must observe multiple vertical levels simultaneously.
For example, when inspecting a tall electrolytic capacitor mounted next to low-profile SMD components, an operator may need to evaluate:
- The solder fillet at the PCB surface
- The lead connection area
- The capacitor body condition
- The surrounding component clearance
However, a conventional microscope can only focus clearly on a limited vertical area.
If the operator focuses on the solder joint, the top of the capacitor becomes blurred. If the focus moves upward to the capacitor body, the solder connection loses sharpness.
This optical limitation becomes more obvious as magnification increases.
Why Depth of Field Becomes the Limiting Factor
Depth of field is the range in which objects appear acceptably sharp under a microscope.
In general:
- Higher magnification provides more detail
- Higher magnification reduces depth of field
This creates a practical conflict during PCB inspection.
| Magnification Level | Typical Application | Depth of Field Challenge |
|---|---|---|
| 5X–10X | General PCB overview | Relatively large focus range |
| 10X–30X | SMT solder inspection | Moderate focus limitation |
| 30X–80X | Fine solder joints and defects | Very shallow focus |
| 100X+ | Micro-level analysis | Extremely limited focus range |
For semiconductor packages, fine-pitch connectors, and solder joint inspection, engineers often require higher magnification to identify defects. However, the increased magnification can make three-dimensional inspection more difficult.
This is why simply purchasing a higher magnification microscope does not always improve PCB inspection efficiency.
The key question is not:
“How much magnification can the microscope provide?”
The more important question is:
“Can the microscope maintain clear focus across the height differences of the components being inspected?”
The Cost of Manual Refocusing During PCB Inspection
With traditional stereo microscopes and standard digital microscopes, operators often need to manually adjust focus when moving between different inspection areas.
For simple PCBs, this may not create significant problems. However, for complex assemblies containing hundreds of components, repeated focusing creates several challenges:
Reduced Inspection Efficiency
Constant refocusing interrupts the inspection workflow. Engineers spend additional time adjusting the microscope instead of evaluating defects.
Inconsistent Inspection Results
Different operators may focus on different areas of a component, creating variation in inspection judgment.
Increased Risk of Missing Defects
Small cracks, incomplete solder wetting, solder bridges, or lead alignment problems may remain unnoticed when important areas are out of focus.
Difficult Documentation
A blurred image is not suitable for:
- Quality reports
- Supplier communication
- Failure analysis records
- Customer approval documents
For electronics manufacturers and inspection service providers, consistent image quality is becoming increasingly important as traceability requirements continue to increase.
4 Critical Tall Component Inspection Scenarios on Modern PCBAs
Modern electronics manufacturing includes many applications where component height creates inspection difficulties. The following scenarios represent some of the most common challenges faced by engineers.
1. Tall Connectors and PIN Coplanarity Inspection
Connectors are among the most challenging PCB components because they combine mechanical height, multiple pins, and strict alignment requirements.
Common inspection targets include:
- Pin coplanarity
- Bent terminals
- Incomplete solder joints
- Solder bridging
- Connector alignment
- Insertion depth
For example, USB connectors, board-to-board connectors, and industrial communication interfaces often have pins located several millimeters above the PCB surface.
A conventional microscope may clearly show the connector housing but fail to maintain focus on both the upper mechanical structure and the solder joints underneath.
An EDF microscope allows engineers to capture a fully focused image of the entire connector structure, making it easier to evaluate both mechanical and solder-related issues.

2. Electrolytic Capacitors and Power Inductors: Solder Fillet Inspection
Power components often have larger dimensions compared with standard SMT devices.
Examples include:
- Aluminum electrolytic capacitors
- Power inductors
- Transformers
- Chokes
During inspection, engineers need to evaluate:
- Solder fillet formation
- Lead wetting quality
- Component tilt
- Cracks caused by mechanical stress
- Thermal damage
The challenge is that the solder connection is located near the PCB surface, while the component body extends significantly upward.
A microscope with insufficient depth of field may require multiple focus adjustments between the component top and solder area.
For high-reliability applications such as automotive electronics, industrial control systems, and power electronics, maintaining clear visibility of the complete component structure is essential.

3. Shield Cans and Heat Sinks: Clearance and Surface Inspection
Metal shielding covers and heat sinks introduce another inspection challenge because they create both height differences and reflective surfaces.
Typical inspection tasks include:
- Checking shielding cover installation
- Measuring clearance between components
- Inspecting solder points around shield edges
- Identifying mechanical damage
- Evaluating thermal interface areas
Reflective metal surfaces can also create glare problems under standard illumination.
Advanced PCB inspection microscopes often combine adjustable lighting systems with image processing technologies to improve visibility on reflective surfaces.
4. Stacked Modules and Multi-Level PCB Assemblies
Modern electronic products increasingly use stacked structures to save space.
Examples include:
- 3D electronic modules
- Multi-board assemblies
- Memory stacking structures
- High-density power modules
These designs create inspection requirements similar to miniature mechanical assemblies.
Engineers may need to observe:
- Multiple PCB layers
- Vertical spacing
- Component alignment
- Interconnection points
- Height differences between structures
Traditional microscopy becomes less effective because different levels cannot remain simultaneously sharp.
EDF imaging provides a practical solution by combining information from multiple focus planes into one comprehensive image.

What to Look For: Key Features Needed for Tall Component Inspection
Choosing the right microscope for inspecting tall PCB components requires more than evaluating magnification or camera resolution. For complex PCB assemblies, the most important factors are related to focus capability, optical accessibility, viewing flexibility, and measurement performance.
A suitable PCB inspection microscope should help engineers answer several practical questions:
- Can the system keep both low solder joints and tall components in focus?
- Can operators inspect difficult areas without damaging components?
- Can images be documented and reviewed consistently?
- Can the system provide measurable data instead of only visual judgment?
The following features are especially important when selecting a microscope for tall component inspection.
1. Extended Depth of Field (EDF) and Focus Stacking Technology
Extended Depth of Field (EDF), also known as focus stacking, is the most important technology for inspecting PCB assemblies with large height variations.
Traditional microscopes capture a single optical plane. If a component extends beyond the available depth of field, only part of the object appears sharp.
EDF microscopes solve this problem by capturing multiple images at different focus positions and combining the sharp areas from each image into one fully focused result.
The basic workflow includes:
Step 1: Multi-Level Image Capture
The microscope captures images at different Z-axis positions, from the lowest inspection area to the highest component surface.
Step 2: Sharpness Analysis
The software analyzes each image layer and identifies the areas with the highest detail.
Step 3: Image Fusion
The sharp regions from different focal planes are combined into a single image.
Step 4: Complete Inspection View
The final image shows multiple height levels clearly in one frame.
For PCB inspection, this provides several advantages:
- Clear solder joints and component bodies simultaneously
- Reduced manual focusing operations
- More consistent inspection results between operators
- Better quality documentation
- Easier defect comparison
Unlike digital sharpening filters, EDF technology uses optical information from different focal planes, making it more suitable for true three-dimensional inspection environments.

2. Long Working Distance (LWD) Optics for Tall Components
Working distance is another critical factor when inspecting tall electronic components.
Working distance refers to the space between the microscope objective lens and the inspection surface when the image is in focus.
A short working distance can create several problems:
- The lens may collide with tall components
- Limited space for soldering tools or probes
- Difficult access to large PCBs
- Restricted viewing angles
For PCB inspection applications, long working distance optics provide additional clearance between the lens and the assembly.
This is particularly important for:
- Through-hole components
- Large connectors
- Power modules
- Automotive PCB assemblies
- Industrial control boards
A microscope with appropriate working distance allows engineers to inspect, repair, and manipulate components more comfortably without moving or damaging the board.
3. Oblique Viewing Angle and 3D Observation Capability
Many PCB defects cannot be evaluated from a vertical top view alone.
For example:
- Solder fillet quality
- Lead lifting
- Sidewall cracks
- Connector alignment
- Component deformation
These defects are often located on vertical or angled surfaces.
An inspection system with adjustable viewing angles allows operators to observe components from different directions.
Benefits include:
- Better visibility of side solder joints
- Reduced shadowing
- Improved understanding of component geometry
- More accurate defect evaluation
For high-density PCB assemblies, the ability to rotate or tilt the observation angle can be as important as magnification.
A microscope that only provides a top-down view may miss critical information hidden behind tall components.
4. Large Field of View (FOV) and High-Clearance Stand Design
Field of view (FOV) determines how much of the PCB area can be observed in one image.
A larger field of view improves efficiency when inspecting:
- Complete PCB assemblies
- Large motherboards
- Power electronics
- Industrial controllers
- Multi-component areas
A narrow field of view forces operators to constantly move the microscope, reducing inspection speed.
For tall component inspection, the mechanical structure is equally important.
A high-clearance stand provides:
- Space for large PCBs
- Flexible component positioning
- Easier access during repair
- Compatibility with different fixtures
For electronics manufacturers and inspection laboratories handling various PCB sizes, optical performance and mechanical flexibility should be considered together.
5. Adjustable Lighting for Reflective and Complex PCB Surfaces
Lighting plays a major role in detecting PCB defects.
Many electronic components contain reflective surfaces, including:
- Metal shielding covers
- Connector contacts
- Solder joints
- Ceramic packages
- Polished terminals
Poor illumination can create:
- Strong reflections
- Hidden defects
- Low contrast images
A professional PCB inspection microscope should support flexible illumination options, such as:
Ring Light
Provides general illumination for standard PCB inspection.
Coaxial Illumination
Useful for reflective surfaces because light is directed along the optical axis.
Polarized Lighting
Helps reduce glare on highly reflective materials.
Proper lighting design improves image consistency and reduces dependence on operator experience.
Why an Extended Depth of Field (EDF) Microscope Is the Ultimate Choice for Tall Component Inspection
When inspecting tall PCB components, the biggest challenge is not simply seeing smaller details. It is maintaining complete visual information across different heights.
This is where EDF microscopes provide a significant advantage.
Traditional optical systems require a compromise:
- Focus on the solder joint → component body becomes blurred
- Focus on the component body → solder area loses detail
EDF technology removes this compromise by combining multiple focus layers into a single sharp image.
For applications such as SMT inspection, connector analysis, semiconductor packaging, and electronic failure analysis, this approach provides a more complete understanding of the assembly.
2D Visual Inspection vs. EDF Imaging: Key Differences
| Inspection Requirement | Traditional Stereo / Digital Microscope | EDF Microscope |
|---|---|---|
| Single focal plane observation | Excellent | Excellent |
| Tall component inspection | Limited | Excellent |
| Multiple height levels in focus | Difficult | Automatic |
| Manual focusing required | Frequent | Reduced |
| Image documentation | Good | Excellent |
| Solder joint and component body visibility | Often requires refocusing | Visible together |
| Operator dependency | Higher | Lower |
| Suitable for complex PCBA | Moderate | High |
EDF Microscope Applications in PCB Manufacturing and Inspection
EDF microscopes are commonly used in applications where component height variation affects inspection quality.
Typical applications include:
SMT Assembly Inspection
Inspection of:
- Solder bridges
- Missing components
- Component placement
- Tombstoning
- Solder joint quality
Through-Hole Component Inspection
Inspection of:
- Pin soldering
- Lead forming
- Connector installation
- Mechanical alignment
Semiconductor Package Inspection
Inspection of:
- BGA solder balls
- Package surfaces
- Wire bonding areas
- Mold defects

Electronics Failure Analysis
Inspection of:
- Cracks
- Burn marks
- Contamination
- Mechanical damage
For engineers looking for a complete solution for electronics quality control, a dedicated PCB inspection microscope system provides optimized imaging, measurement, and documentation capabilities for modern circuit assemblies.
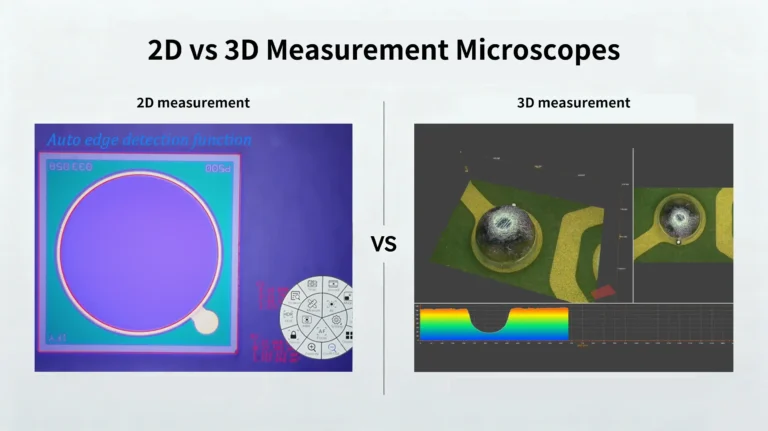
Real-Time 3D Height Profiling: Beyond Simply Seeing Tall Components
For many inspection tasks, visual clarity is only the first requirement.
Engineers increasingly need quantitative information, such as:
- Component height
- Step differences between structures
- Package thickness
- Solder joint dimensions
- Surface profile variation
Advanced 3D measuring microscopes combine optical imaging with measurement algorithms to provide height analysis.
This capability is valuable for applications where dimensional verification is required, including:
- Semiconductor packaging
- Precision electronics manufacturing
- Microelectronic assemblies
- Quality verification processes
Instead of relying only on operator judgment, engineers can obtain measurable inspection data for reports and process improvement.
Conclusion
Inspecting tall components on modern PCB assemblies is no longer simply a matter of increasing magnification. As electronic products become more compact and integrate components with significant height differences, the primary challenge shifts from image resolution to maintaining focus across multiple vertical planes.
Traditional stereo and standard digital microscopes remain valuable for many routine inspection tasks, particularly in PCB repair and general visual examination. However, they often require continuous manual refocusing when inspecting connectors, electrolytic capacitors, power inductors, shield cans, and stacked assemblies. This not only slows the inspection process but can also lead to inconsistent results between operators.
Extended Depth of Field (EDF) microscopes address this challenge by combining multiple focal planes into a single fully focused image. The result is a clearer view of solder joints, component bodies, and surrounding structures without sacrificing image quality. For electronics manufacturers, quality engineers, and inspection laboratories, this translates into faster inspections, improved documentation, and greater confidence when evaluating complex PCB assemblies.
When selecting a microscope for tall component inspection, focus on the overall inspection workflow rather than magnification alone. Features such as Extended Depth of Field, long working distance optics, flexible illumination, large field of view, and integrated measurement tools have a far greater impact on productivity and inspection accuracy in real-world applications.
As PCB designs continue to evolve toward higher density and more three-dimensional architectures, microscope systems capable of delivering both comprehensive visualization and reliable measurement will become increasingly important for maintaining product quality and manufacturing consistency.